 Spain
 English
 France
Ice Cream Cup Condensation: A Buyer’s Control Guide
Learn why ice cream cup condensation forms, how it differs from leakage, and what buyers should test in coatings, lids, storage and delivery.
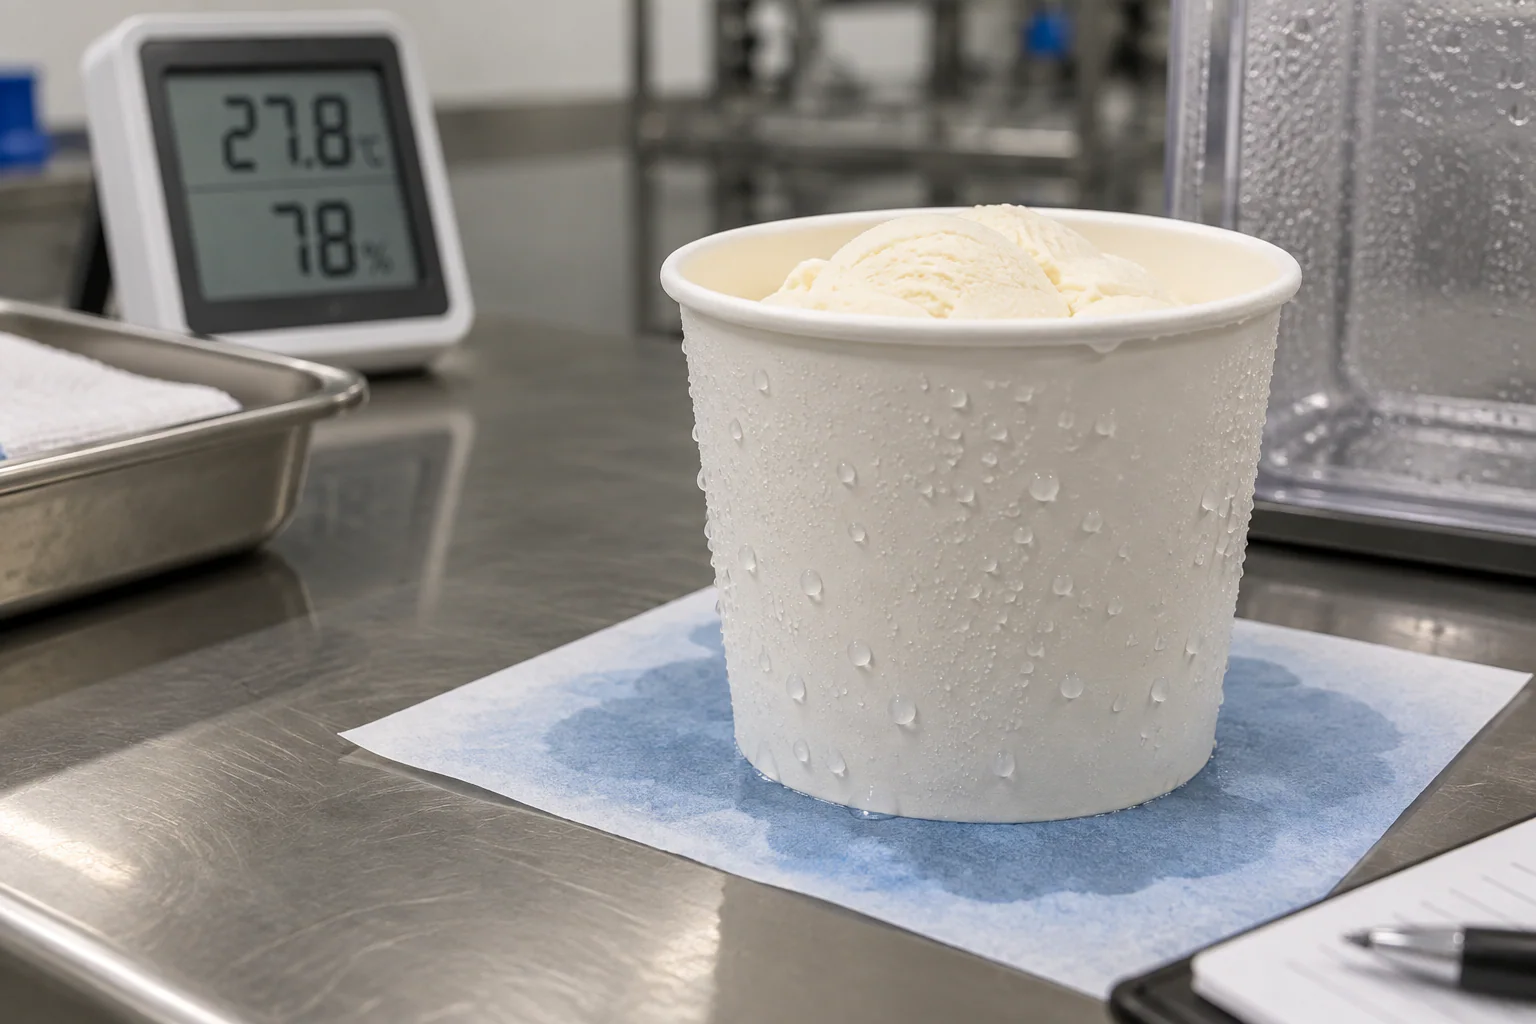
Ice cream cup condensation is moisture from the surrounding air that forms on a cold package surface; it is not automatically a leak from inside the cup. When a frozen dessert cup moves from cold storage into warmer, humid air, the outer wall and lid can become cold enough for water vapor to condense into droplets. Those droplets may soften exposed paper fibers, wet a carrier, mark printed surfaces or collect around the cup base.
For buyers, the solution is not a generic “waterproof” claim. The cup, outer barrier, lid, portion, storage sequence, ambient environment and delivery pack need to be evaluated as one system. This guide explains the decisions and sample checks that help control condensation without inventing universal hold times or performance guarantees.
Why does ice cream cup condensation form?
Air contains water vapor. When that air contacts a sufficiently cold cup, the air next to the surface cools. If the surface is below the air’s dew point, some vapor changes into liquid water on the outside of the package. The same effect appears on a cold bottle or glass.
The amount and speed of condensation depend on the complete use environment:
- temperature of the frozen dessert and cup;
- ambient temperature and relative humidity;
- time outside cold storage;
- air movement around the package;
- cup geometry and filled mass;
- exterior surface construction;
- contact with carriers, bags and neighboring cups.
A supplier cannot responsibly promise one condensation result for every market. A cup used in a dry, air-conditioned shop faces a different environment from the same cup carried through a humid summer street.
Condensation or leakage? Diagnose the moisture source first
Condensation begins on the outside. Leakage originates from product passing through or around the package. The two can look similar after water collects at the base, so buyers should isolate the source before changing materials.
| Observation | Likely question | Useful check |
|---|---|---|
| Fine droplets across the full outer wall | Is warm humid air meeting a cold surface? | Compare an empty room-temperature control with a chilled filled sample. |
| Wet line at the side seam | Is moisture following a seam or only collecting there? | Dry the exterior, place it on a fresh indicator sheet and observe the seam. |
| Localized dark patch growing from inside | Is the barrier damaged or discontinuous? | Inspect coating, cut edges and seam areas under bright light. |
| Moisture around the rim | Is the cup overfilled or the lid mismatched? | Check filled height, rim diameter and lid engagement. |
| Wet carrier with intact cup wall | Are exterior droplets being transferred to the pack? | Test the complete cup-and-carrier configuration. |
Labeling every wet base as a “leak” can lead to the wrong correction. A seam defect may require forming-process work, while exterior condensation may require an outer barrier, different handling sequence, sleeve, carrier ventilation or shorter exposure.
How double PE affects ice cream cup condensation
The currently confirmed construction for GLY PACK’s general-purpose ice cream bowls is coated C1S white paperboard with double PE and a 240 gsm board baseline. Larger sizes may require higher GSM, which must be confirmed for the actual format and filled weight.
Double PE means a polyethylene barrier is applied to both sides of the paperboard. The internal layer separates the dessert from the fibers. The external layer helps prevent condensed water from directly wetting the outside paper surface. This is why an exterior coating is relevant to frozen products even when the product itself only contacts the inside.
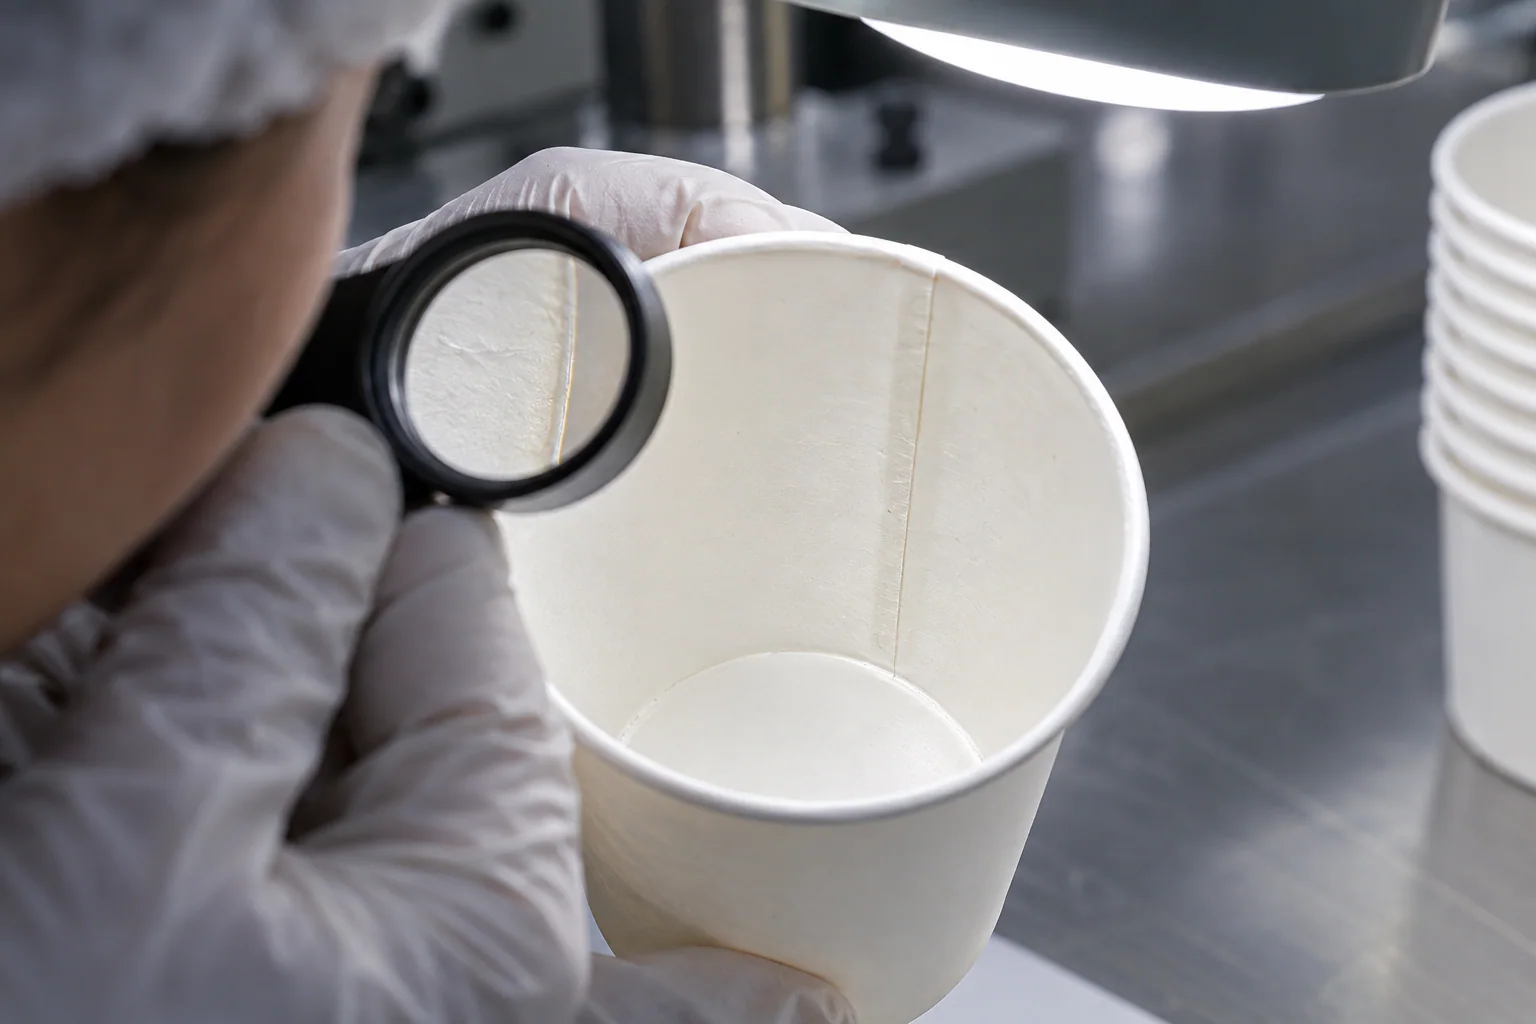
Double PE does not stop condensation from forming; it manages how the package responds to the droplets. Water may still bead on the outside. Finished performance also depends on coating continuity, forming, cut edges, rim construction and physical damage.
Paperboard surface and GSM serve different functions
Uncoated white board generally appears more matte. Coated C1S white paperboard has a smoother, brighter printing surface. That surface treatment affects appearance and ink presentation, while the PE layers provide the stated moisture-barrier construction. Buyers should avoid treating “coated paper” as a complete barrier specification because the word “coated” may refer to the printable mineral-coated surface rather than the polymer moisture layer.
GSM describes basis weight, not waterproofness. A heavier board may improve stiffness for a larger or heavier portion, but simply increasing GSM does not replace a continuous barrier. Specify both the board and the coating.
Cup size, filled mass and lid fit change the result
A larger filled package carries more cold mass and presents a different surface area to the surrounding air. Geometry also affects where droplets run and collect. GLY PACK’s confirmed general-purpose bowl references are:
| Approx. capacity | Rim diameter | Bottom diameter | Height | Lid |
|---|---|---|---|---|
| 100 ml | 75 mm | 60 mm | 45 mm | Transparent lid |
| 200 ml | 85 mm | 70 mm | 50 mm | Transparent lid |
| 250 ml | 95 mm | 80 mm | 55 mm | Transparent lid |
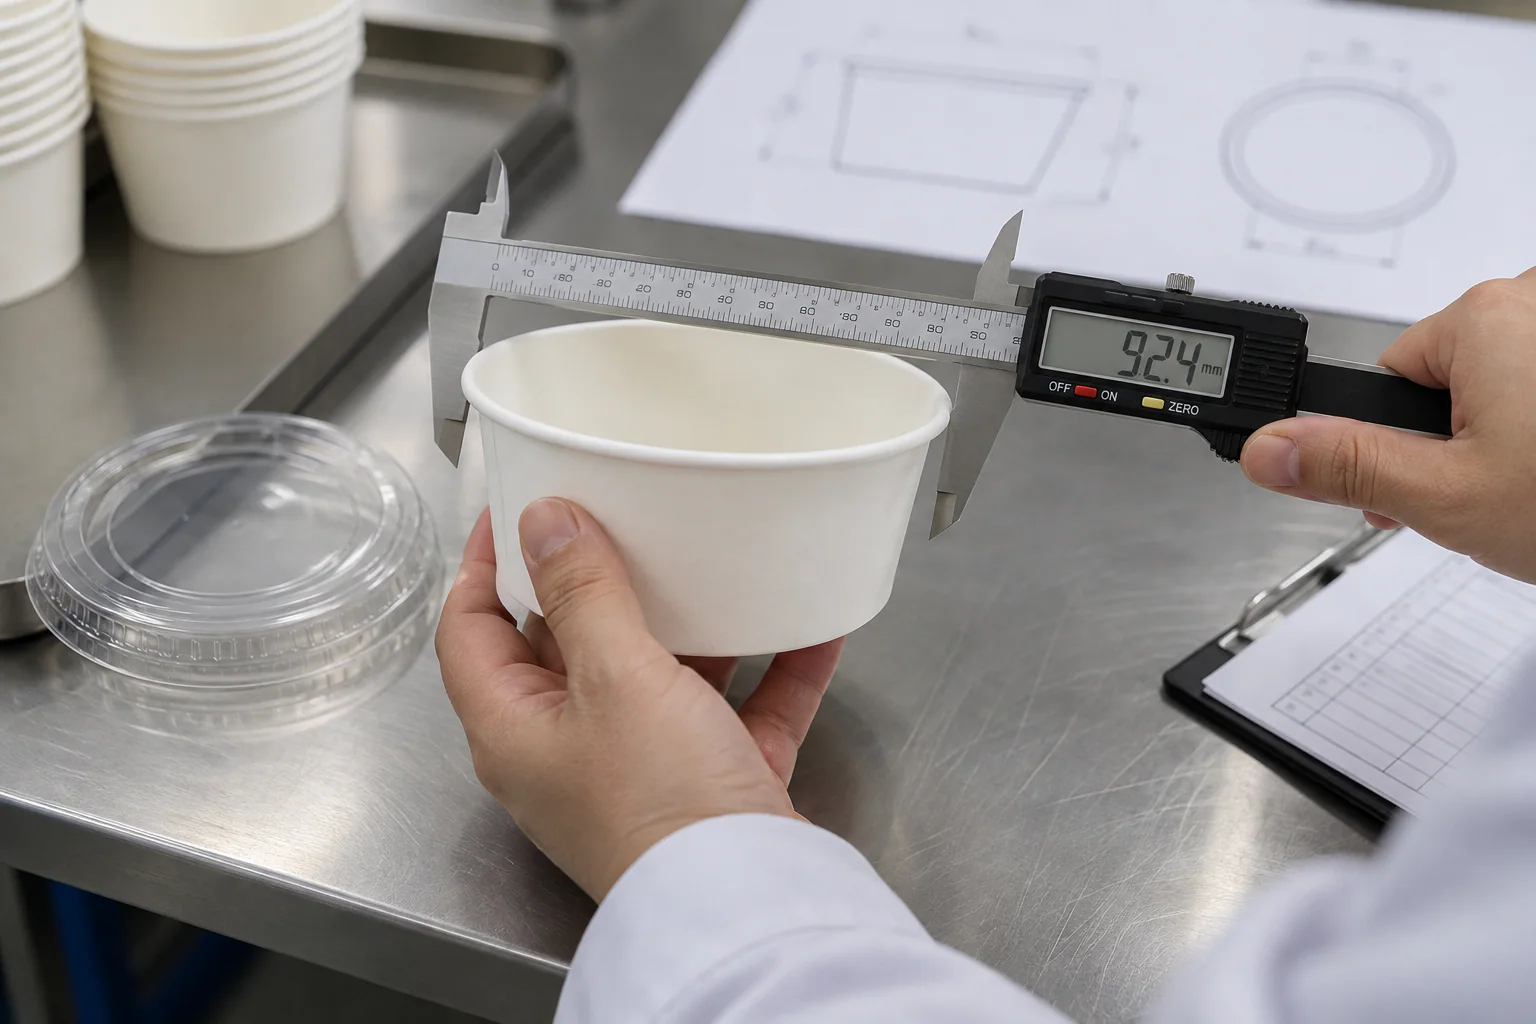
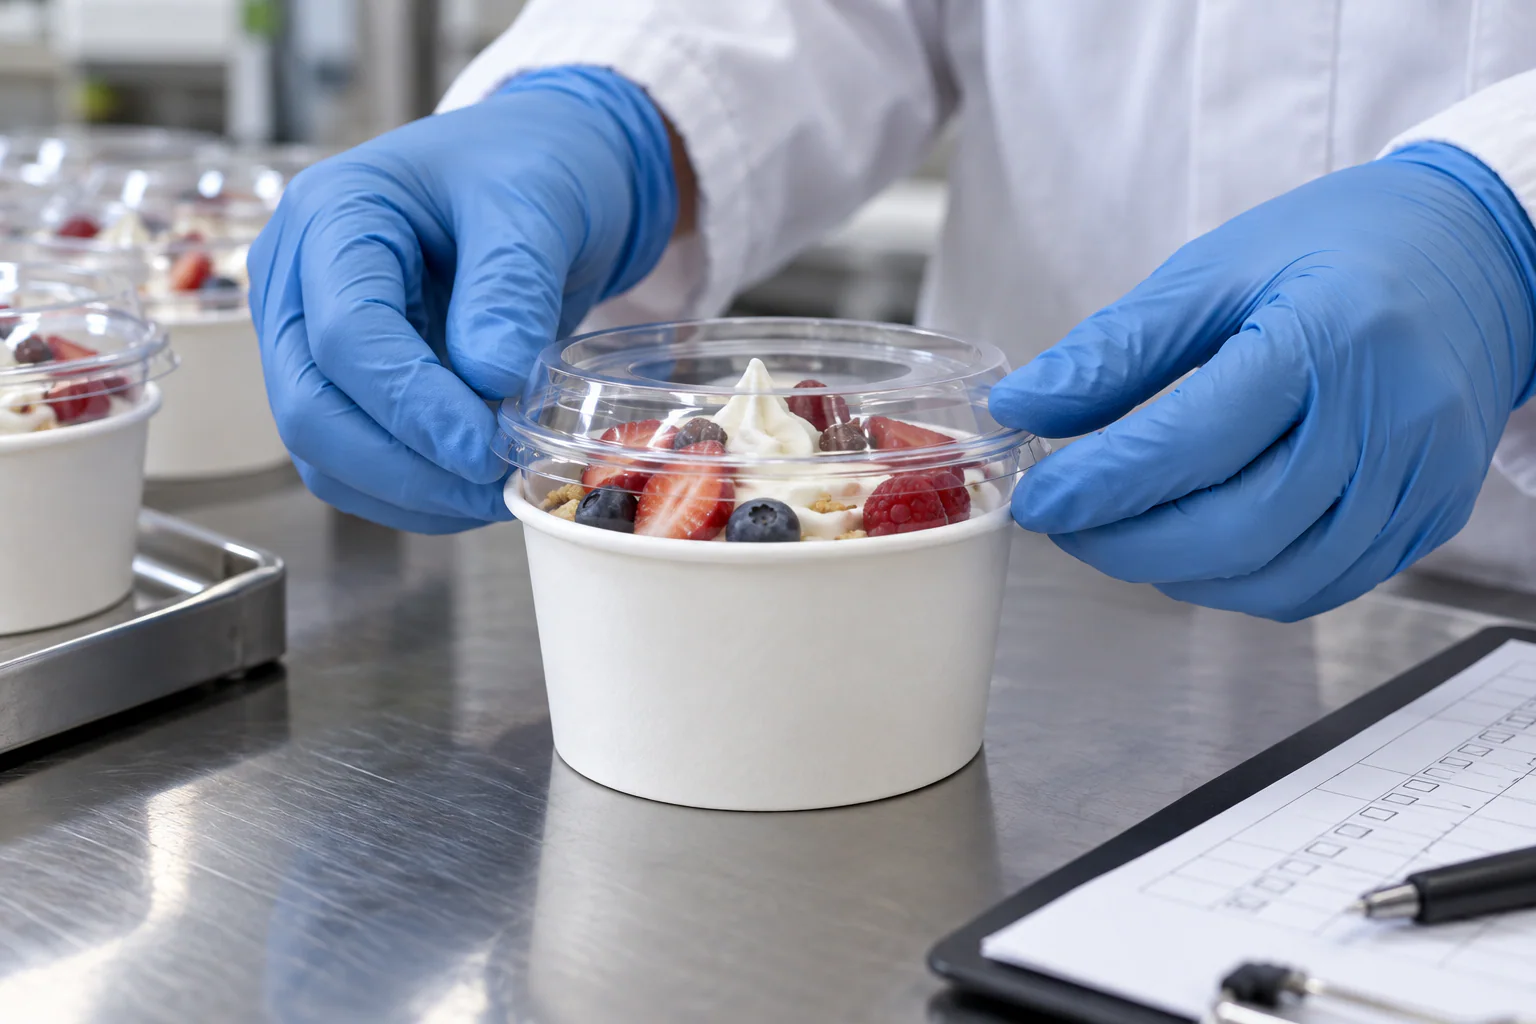
Measure samples rather than relying only on nominal capacity. A lid gap may allow product to reach the rim, while an overfilled dessert can transfer sauce or toppings to the lid. Neither should be confused with water condensing on an otherwise sealed outside surface.
A practical ice cream cup condensation test workflow
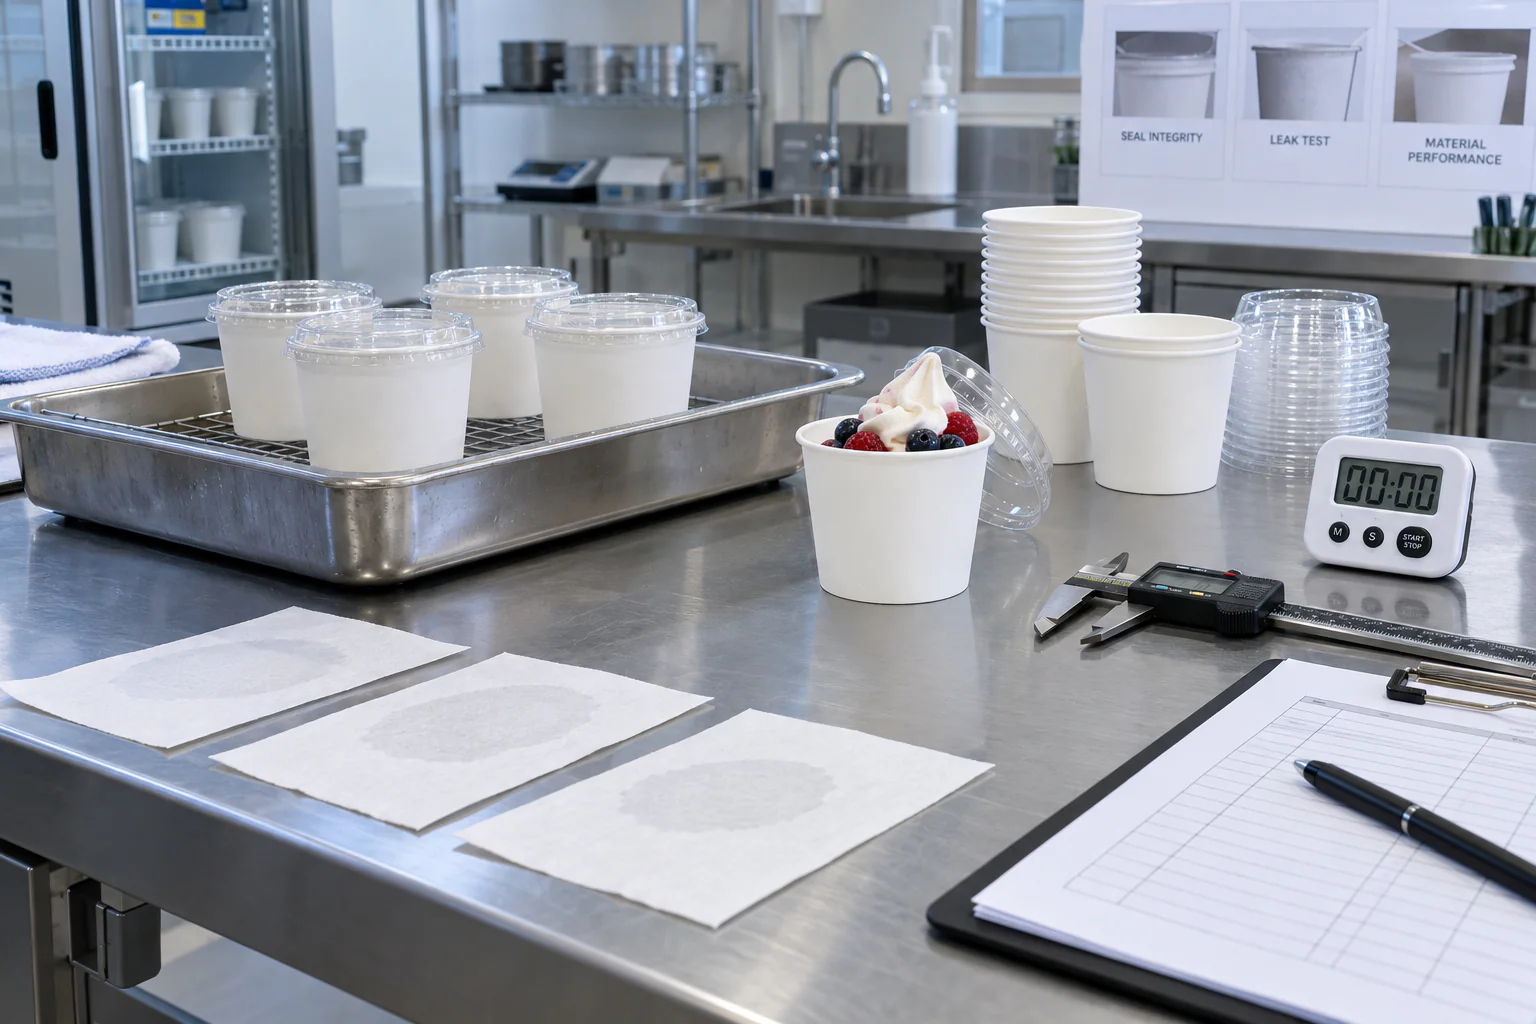
The following workflow is suitable for supplier samples and buyer-side trials. The buyer should define the actual temperature, humidity, duration and acceptance criteria for its market.
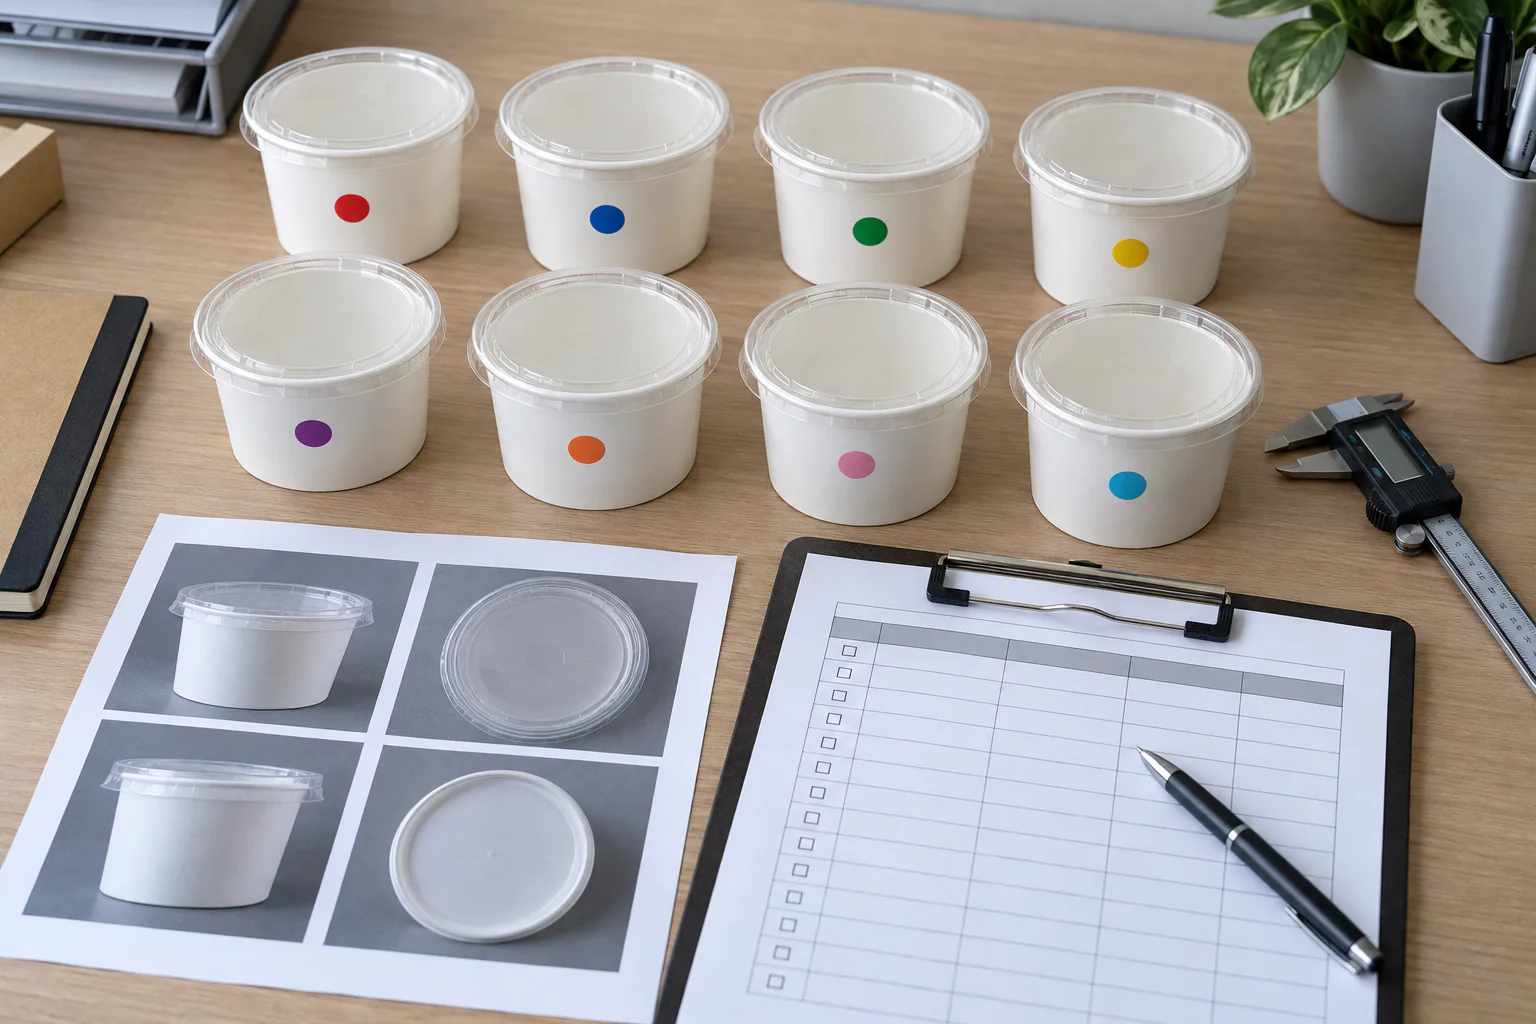
- Record the sample: cup size, board, coating, lid, artwork, sample date and source.
- Inspect it dry: photograph the wall, rim, side seam and base before exposure.
- Prepare controls: keep an empty room-temperature cup and an unexposed cup for comparison.
- Fill with the real dessert: include normal toppings and both normal and high-fill portions.
- Use the intended cold-storage sequence: test the same transition expected in operation.
- Place samples on clean indicator sheets: separate samples so transferred moisture is visible.
- Observe at planned intervals: record droplets, surface darkening, softening, print change and pooled water.
- Repeat in the carrier: test cups touching dividers, bags or neighboring packs.
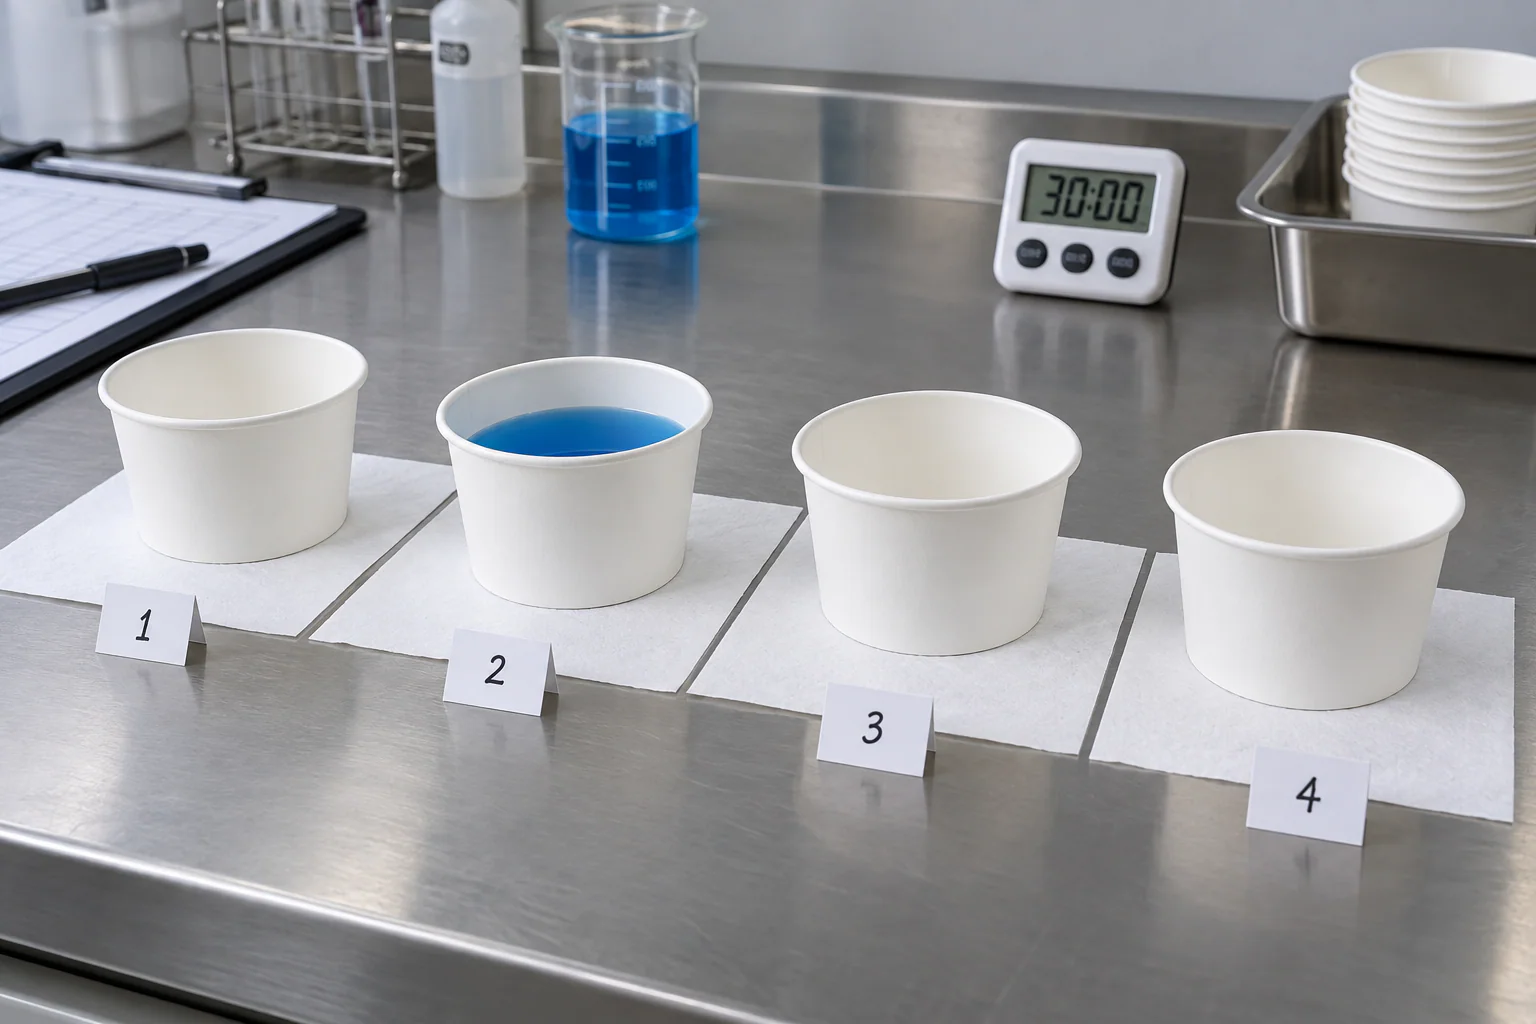
Do not change cup size, dessert, storage time and ambient condition simultaneously if the objective is to identify a cause. A simple test matrix produces more useful evidence than one dramatic demonstration.
Test the delivery carrier, not only the cup
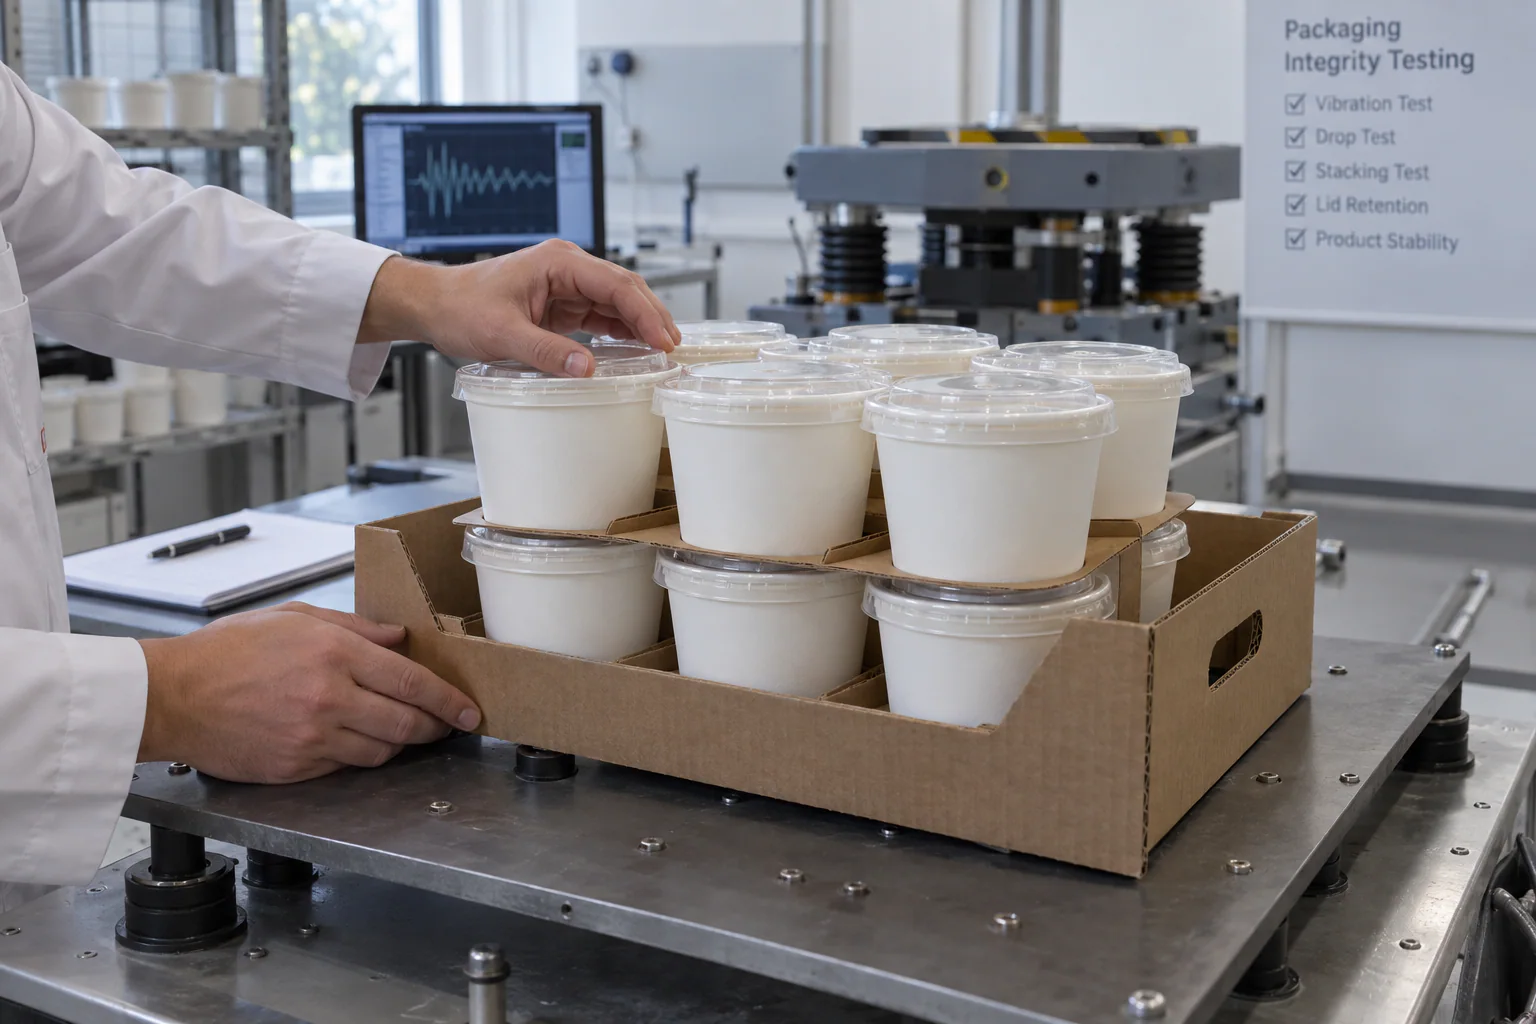
Condensation may move from the cup into a cardboard divider, bag or carton. That can reduce pack stiffness, create stains or allow cups to shift. Test the complete packed order with the intended number of cups, accessory placement and stacking pattern. Inspect contact points after the route simulation.
Accessories should also match the packaging plan. GLY PACK’s confirmed accessory set includes flat lids, dome lids, transparent spoons, black forks and natural wood spoons, with a confirmed accessory minimum of 200 pieces subject to compatibility and quotation.
Use paper tests correctly
Material tests can help compare paperboard, but they do not simulate a finished frozen-dessert package. ISO 535:2023 specifies the Cobb method for water absorptiveness of paper and board under standard conditions. TAPPI/ANSI T 441 om-24 describes a related standardized Cobb procedure for sized paper, paperboard and corrugated fiberboard.
Those methods characterize material behavior. A finished cup adds barrier layers, seams, rim and bottom forming, printing, lids, cold storage and handling. Use laboratory data as one evidence layer, then test the completed package.
Food-contact compliance is separate from condensation control
Food-contact documentation and condensation performance answer different questions. The U.S. FDA explains that packaging components, coatings, adhesives and colorants may be food-contact substances and that authorization depends on intended use. See the FDA’s official food-packaging overview.
For Europe, the European Commission states that food-contact materials must follow Regulation (EC) No 1935/2004 and applicable good-manufacturing-practice rules. Its food-contact materials page is a useful regulatory starting point. Ask for documents that match the exact paperboard, PE layers, inks, adhesives, food type and conditions of use.
What buyers should place in the RFQ
- dessert type, portion weight, toppings and filled height;
- cup capacity and critical dimensions;
- paperboard surface, basis weight and internal/external barrier construction;
- lid style, material, diameter and required headspace;
- cold-storage condition and expected time in warmer air;
- destination climate and delivery method;
- acceptance criteria for softening, staining, print transfer and lid retention;
- food-contact documents required by the destination market;
- sample and repeat-test requirements before bulk approval.
Frequently asked questions
Does condensation mean an ice cream cup is leaking?
No. Condensation forms from moisture in the surrounding air on a cold outside surface. Leakage originates from the product passing through a barrier, seam, rim or lid. Drying the exterior and observing the sample on a fresh indicator sheet helps separate them.
Will double PE stop condensation?
No. It does not prevent water vapor in the air from becoming droplets. The exterior PE layer helps protect the paperboard from direct exposure to those droplets as part of the specified moisture-barrier construction.
Is heavier paperboard always better?
Higher GSM can add stiffness when a larger package or heavier portion needs it, but it does not replace a continuous moisture barrier or correct forming. Confirm both GSM and coating for the actual size.
Why test the carrier?
Water can transfer from the cup to dividers, bags and cartons. Several cold cups together can create a different moisture environment from one cup tested alone. The complete pack therefore needs evaluation.
Can one climate test represent every market?
No. Ambient temperature, humidity, air movement and service time vary. Use the conditions of the intended market and route, and record them with the result.
Control ice cream cup condensation with a complete specification
Effective condensation control combines an appropriate internal and external barrier, sufficient board stiffness, compatible lids and a tested cold-to-warm handling sequence. Review GLY PACK’s paper bowl range, then share your dessert, cup size, lid and service environment. The objective is a sample approval tied to real operating conditions—not an unsupported “waterproof” promise.